How to Choose the Best Underpad Machine in 2026?
Choosing the best underpad machine in 2026 requires more than comparing prices and production speeds. A reliable decision begins with your actual product requirements, factory space, labor capacity, and quality targets. The right machine should handle different underpad sizes, absorbent core materials, and packaging formats without constant adjustments.
Look closely at key details. Check the forming system, cutting accuracy, sealing performance, and production stability. Ask how quickly the machine reaches its rated output. A practical test should measure waste, downtime, noise, and changeover time. These details often matter more than impressive brochure figures. Experienced operators can also reveal problems that specifications may hide, such as difficult cleaning points or frequent sensor alarms.
A trustworthy underpad machine supplier should provide clear technical documents, training, spare parts, and responsive service. Verify electrical standards, safety features, installation requirements, and documented quality controls before signing a contract. Independent testing and customer references can strengthen your assessment. Still, no machine is perfect for every factory. Production estimates may change after installation. My own review process would include more long-term data than many buyers can access, so some conclusions deserve careful checking. A lower purchase price may become expensive when maintenance, material waste, and downtime accumulate. Choose a system that supports consistent hygiene products, measurable efficiency, and realistic growth in 2026.
Understanding Underpad Machines and Their Main Functions
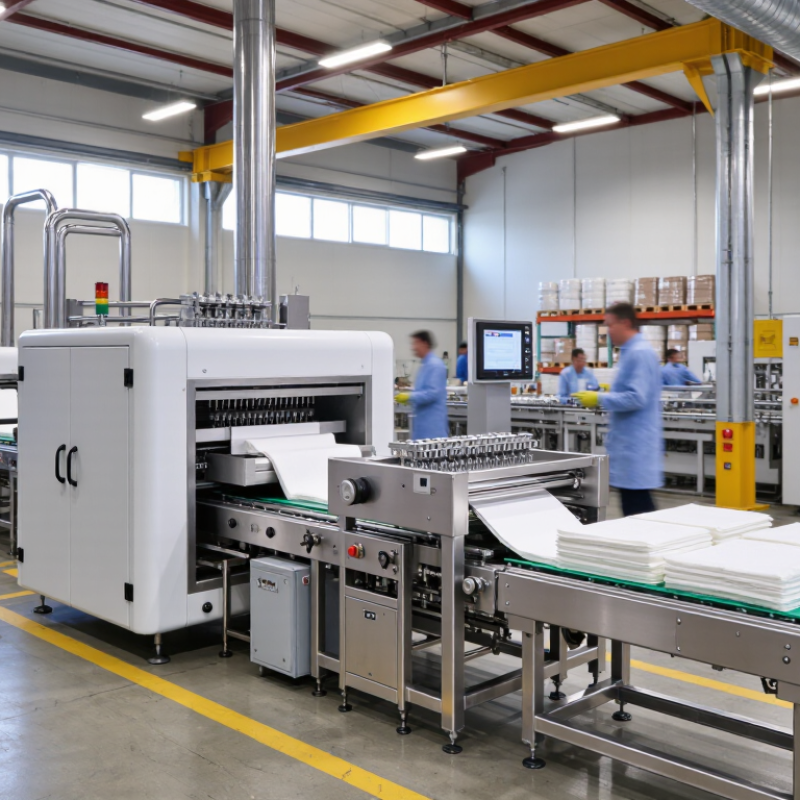
An underpad machine converts rolls of tissue, nonwoven fabric, absorbent pulp, and superabsorbent material into protective bedding pads. It unwinds each material, controls tension, and aligns the layers before forming the absorbent core. At its core, it builds consistency.
The main functions include pulp defibration, material dosing, folding, embossing, sealing, cutting, and stacking. Some machines also use sensors to check pad length, edge position, and missing materials. A clean production area matters because dust can affect seals and sensor accuracy. In 2026, digital monitoring can show speed, stoppages, waste, and maintenance warnings on one screen. Useful, but not magic. Operators still need practical training.
When choosing equipment, compare the required pad sizes, hourly output, changeover time, and available floor space. Check whether the machine handles your preferred material widths and absorbent structure. Servo controls may improve positioning, while automatic tension adjustment can reduce wrinkles. Ask for trial production with your actual materials. A sample pad may look acceptable, yet fail during compression or liquid testing. I once focused too heavily on maximum speed. That judgment was incomplete. Stable feeding and easy cleaning often protect productivity better than a higher advertised rate. Examine guarding, emergency controls, spare-part access, and service documentation before purchase. A reliable machine should be measurable, maintainable, and understandable to the people operating it.
Identifying Production Needs, Materials, and Capacity Requirements
How to Choose the Best Underpad Machine in 2026?
Choosing an underpad machine starts with the product you actually plan to make. A clinic may need compact pads for daily patient care, while a distributor may require larger sizes and faster changeovers. Measure your target pad length, width, absorbent core thickness, and packaging format. Small details matter. A 10-millimeter size variation can affect stacking, sealing, and storage.
Material selection should match the machine’s forming and sealing system. Common structures include nonwoven topsheets, absorbent fluff or pulp cores, waterproof back sheets, and adhesive layers. Test each material under real production conditions. Some films wrinkle near the sealing rollers. Some nonwoven fabrics stretch during feeding. These problems may not appear in a sample trial. Ask for documented test results, material compatibility data, and maintenance records before making a decision.
Capacity requirements should reflect realistic demand, not an impressive maximum speed. Review hourly output, operator needs, changeover time, power use, and scrap rates. A machine rated for 400 pieces per minute may produce much less with thicker cores or frequent size changes. I have seen production plans fail because waste was estimated too optimistically. That mistake is easy to repeat. Include trial runs with your actual materials, inspect seal strength, and record downtime. Reliable equipment should offer stable tension control, accessible adjustment points, clear safety systems, and traceable quality checks. Good data beats confident guesses.
| Selection Dimension | Production Requirement | Typical 2026 Planning Range | Recommended Machine Configuration |
|---|---|---|---|
| Product Size | Standard and specialty underpad formats | 450 × 600 mm; 600 × 600 mm; 600 × 900 mm; 800 × 900 mm; 800 × 1800 mm | Select a servo-controlled cutting and folding system with adjustable web width. Confirm the usable forming width before purchasing, especially for large pads. |
| Target Output | Small, medium, or high-volume production | 40–80 pieces/min for entry-level lines; 80–160 pieces/min for medium-speed lines; 160–300 pieces/min for high-speed lines | Match rated speed to the required sellable output. Allow approximately 10–20% capacity margin for material changes, inspection, cleaning, and minor stoppages. |
| Annual Production | Capacity planning based on operating schedule | About 8–20 million pieces/year at 80–160 pieces/min, assuming two shifts and planned downtime | Calculate output using actual operating hours rather than the nameplate speed. Include downtime for roll replacement, maintenance, quality checks, and product changeover. |
| Top Sheet | Liquid acquisition, skin contact, and surface dryness | Hydrophilic nonwoven, commonly about 10–25 g/m² | Use a stable unwinding unit with web-tension control. Choose spunbond or other suitable nonwoven structures according to softness, wet-back, and liquid-transfer requirements. |
| Absorbent Core | Absorption capacity and retention | Fluff pulp, commonly about 100–500 g/m²; superabsorbent polymer may be added according to product design | Specify pulp opening, metering, forming, and dust-control equipment. If superabsorbent polymer is used, require accurate dosing and uniform distribution across the core. |
| Back Sheet | Leak prevention and surface protection | PE film commonly about 15–35 μm, or a breathable laminated film/nonwoven structure | Choose film unwinding and heat-sealing components compatible with the selected back-sheet material. Check sealing temperature, pressure, dwell time, and film shrinkage. |
| Product Thickness | Flat, lightly embossed, or bulky absorbent structure | Approximately 2–12 mm, depending on core weight, compression, and embossing design | Use adjustable compression, embossing, and folding settings. Confirm that the forming section can handle the maximum core thickness without uneven edges or deformation. |
| Material Width | Roll stock compatibility and material utilization | Common roll widths are approximately 600–2200 mm, depending on the number and size of lanes | Select an unwind stand that supports the required roll diameter, core diameter, roll weight, and web width. A wider working width can improve material utilization for multi-lane production. |
| Machine Speed | Stable continuous operation | Approximately 80–250 m/min web speed for many converting applications | Prioritize stable speed, registration accuracy, and low waste over maximum empty-line speed. Servo drives and automatic tension control are useful for consistent cutting and sealing. |
| Electrical Supply | Factory power compatibility | Common configurations include 380–415 V, three-phase, 50 Hz; total installed power often falls around 30–120 kW | Verify local voltage, frequency, short-circuit protection, transformer capacity, and peak starting load. The final electrical requirement depends on line speed, dust extraction, compressors, and auxiliary equipment. |
| Compressed Air | Pneumatic cylinders, valves, and material handling | Typically about 0.6–0.8 MPa supply pressure; consumption often varies from 0.5–2.0 m³/min | Provide clean, dry, oil-controlled compressed air with sufficient receiver capacity. Confirm consumption at the maximum operating speed, not only at idle conditions. |
| Dust Control | Fluff pulp dust management and workplace cleanliness | Dedicated filtration and extraction are normally required for pulp-forming sections | Specify an enclosed forming area, ducted extraction, filter monitoring, and accessible cleaning points. Dust-control capacity should be matched to pulp throughput and line speed. |
| Cutting Accuracy | Consistent product length and clean edges | Typical target tolerance is approximately ±2–5 mm, subject to material elasticity and machine design | Choose servo-driven length control, automatic registration correction, and rigid rotary or guillotine cutting components. Validate accuracy using the actual top sheet, core, and back-sheet combination. |
| Sealing Method | Reliable bonding between layers | Heat sealing, ultrasonic sealing, adhesive bonding, or a combination of methods | Select the sealing method according to film type, line speed, edge strength, energy use, and permissible adhesive contact. Test seal integrity after production and storage conditioning. |
| Changeover | Multiple sizes or product specifications | Manual changeover may take about 30–90 minutes; guided or semi-automatic systems can reduce setup time | For frequent size changes, prioritize recipe storage, tool-less adjustments, digital length settings, quick-release guides, and clearly marked changeover positions. |
| Quality Inspection | Detection of missing material, wrinkles, poor seals, and incorrect dimensions | In-line sensors can monitor web breaks, registration, length, edge position, and selected surface defects | Specify automatic reject handling, production counters, alarm history, and data export. Add vision inspection when appearance or print registration is commercially important. |
| Floor Space | Line installation, operation, and maintenance access | Compact lines may require about 20–40 m²; medium and high-output lines commonly require 50–120 m² or more | Reserve additional space for raw-material rolls, finished-product packing, dust collectors, electrical cabinets, walkways, and maintenance access. Check ceiling height for roll loading equipment. |
| Labor Requirement | Line operation, inspection, packing, and material handling | Approximately 2–5 operators per shift for a semi-automatic line; staffing varies with packing automation and material handling | Choose automation according to labor availability and product mix. Automatic counting, stacking, bagging, and pallet handling can reduce repetitive manual work. |
| Waste Rate | Material efficiency and cost control | A well-tuned line may target approximately 2–5% process waste; startup and changeover waste can be higher | Request documented waste calculations based on actual materials. Evaluate edge trim, rejected seals, off-size products, startup losses, and roll-end waste separately. |
| Maintenance | Availability and long-term operating stability | Daily cleaning and inspection, scheduled weekly checks, and periodic replacement of blades, belts, bearings, filters, and sealing components | Select a machine with accessible service points, standardized wear parts, clear maintenance schedules, fault diagnostics, and a practical spare-parts package. |
Comparing Machine Types, Features, and Automation Levels
How to Choose the Best Underpad Machine in 2026?
Choosing an underpad machine starts with the product, not the advertised speed. Manual machines suit small workshops and frequent size changes. Semi-automatic models reduce folding and sealing labor while keeping operator control. Fully automatic lines connect material feeding, cutting, folding, sealing, counting, and stacking. They require higher investment but deliver steadier output during long shifts.
Check the core features closely. Servo-driven feeding can improve length accuracy and reduce material waste. Photoelectric sensors help detect missing cores, misalignment, and film breaks. A programmable control system allows operators to adjust pad size, absorbent pulp quantity, and sealing temperature. Automatic tension control matters when handling thin nonwoven fabric. The machine should also provide guarded moving parts, accessible maintenance points, and clear fault messages.
Speed needs careful judgment. A faster line may create more rejects if the absorbent layer shifts or the edges seal unevenly. In practical production checks, changeover time often matters more than maximum output. Ask for sample testing with your actual materials. Inspect the first and last pads from a batch. Small differences can become expensive. I would not choose a machine based on brochures alone. Operators may also need training, especially with sensor calibration and film alignment. A perfect machine does not exist. The better choice balances automation, product consistency, maintenance skill, floor space, and realistic daily demand.
How to Choose the Best Underpad Machine in 2026?
Comparing machine types, production capacity, labor requirements, changeover time, and automation levels.
Fully automatic lines generally provide the highest output and lowest labor requirement, while semi-automatic systems offer a balance between investment, flexibility, and operating efficiency. The figures shown are representative planning benchmarks for standard underpad production configurations; actual performance depends on product size, absorbent-core design, material specifications, and line configuration.
Evaluating Quality, Safety, Energy Use, and Maintenance
Choosing an underpad machine in 2026 requires more than checking production speed.
Quality begins with stable material feeding, accurate absorbent-core placement, and consistent sealing. During factory trials, inspect ten consecutive products, not one perfect sample. Measure pad dimensions, seal strength, absorbency, and reject rates. ISO 9073 test methods can support repeatable nonwoven evaluations. Small variations matter. They can become visible leaks in real use.
Safety should include guarded moving parts, emergency stops, noise control, and clear maintenance access.
ISO 12100 offers a practical framework for machinery risk assessment. Energy use also deserves close attention. The International Energy Agency reported that industry consumed about 37% of global final energy in its Energy Efficiency 2023 analysis. Compressed air can be another hidden cost; the U.S. Department of Energy notes that it may consume around 10% of industrial electricity. Request measured power data at the actual operating speed, not only rated capacity.
Tips:
Ask for a full-load energy test. Check air leakage with ultrasonic inspection. Review maintenance records, spare-part lead times, and lubrication points. A machine with fewer sensors is not always simpler; poor monitoring may increase waste. Preventive maintenance should cover sealing heaters, cutters, vacuum lines, and tension rollers. Keep a documented calibration schedule. I would also question impressive speed claims, because unstable speed creates more rejects and harder troubleshooting. Reliability is proven by repeatable production, accessible records, and safe daily operation.
Selecting a Reliable Supplier and Calculating Total Ownership Cost
Selecting the best underpad machine in 2026 requires more than comparing purchase prices. Grand View Research valued the global adult incontinence products market at USD 15.7 billion in 2023. It projects a 6.7% compound annual growth rate through 2030. This growth increases pressure on suppliers to deliver stable output, fast changeovers, and dependable after-sales support.
Calculate TCO per usable underpad, not per machine. Include the purchase price, installation, operator hours, spare parts, energy, compressed air, waste, and scheduled downtime. A simple formula helps: annual ownership cost divided by saleable units. Request data from at least three production speeds. Then test quality at low, normal, and peak speed. The formula is useful, but not perfect. Local electricity rates and labor skills can change the result quickly. A cheaper machine may consume more material through edge waste. That hidden cost often appears after commissioning. Ask for documented factory acceptance tests, maintenance intervals, and response times. Quality procedures aligned with ISO 13485 can also indicate stronger process control, although certification alone cannot guarantee machine performance.
Tips: Visit a working installation before signing. Measure absorbency, sealing strength, noise, and scrap for a full shift. Check whether common sensors and blades are locally available. Request a written training plan and spare-parts list. Leave room for mistakes; real production is rarely as smooth as a supplier demonstration.
Related Posts
-
7 Tips for Global Buyers Choosing the Best Underpad Machine?
-
How to Use an Underpad Machine for Efficient Laundry Management?
-
Top Underpad Manufacturing Machine Techniques for Optimal Production Quality?
-
Why Invest in an Underpad Manufacturing Machine for Your Business?
-
How to Choose the Best Underpad Manufacturing Machine?
-
Why Are Manufacturing Machines Essential for Global Sourcing?